Why Does Your Low-Temperature Evaporator Fail After Only Three Months? 90% of Manufacturers Stumble at the 'Feed Water' Step
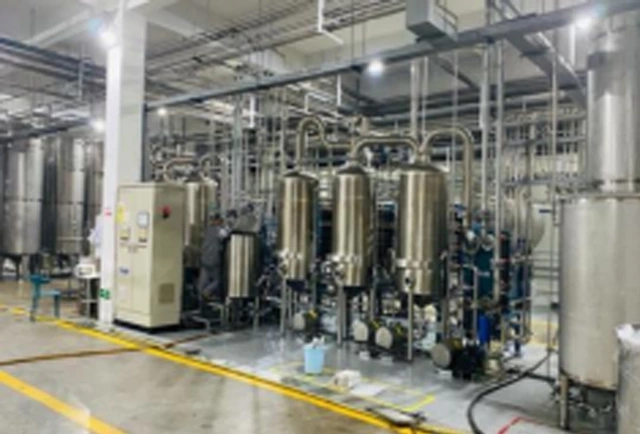
A low-temperature evaporator is not mysterious in principle—it is vacuum distillation: vacuum lowers the boiling point so water evaporates around 40 °C, leaving COD, salts and oil all in the concentrate, with reuse water out and the concentrate consigned—sounding like a 'universal remedy' for high-salt, high-COD wastewater.
But anyone on site knows: the same equipment—some plants run three years without cleaning, while others have the heat-transfer surface caked in three months, the compressor roars and the vacuum pump shakes, with breakdown maintenance more expensive than the equipment itself.
Where is the difference? Not in the equipment, but in what you did to that stream of water before it entered the evaporator.
Below, these 5 types of water quality going straight into low-temperature evaporation = paying for a lesson.
I. Oily Wastewater: Cutting Fluid, Emulsion, Die-Casting Release Wastewater
For feed oil content > 1000 mg/L, de-oiling is mandatory first.
Oil has two faces: floating oil forms an oil film on the heat-transfer surface, halving the heat-transfer coefficient—you either raise the temperature difference (energy up) or clean chemically more often (downtime up); emulsified oil is more insidious, traveling with the foam—foam carries oil droplets into the secondary steam and the condensate is instantly contaminated; one test of the reuse water shows COD higher than some influent indicators.
Pretreatment scheme: oil separation + dissolved-air flotation, or demulsification-coagulation, to push feed oil below 500 mg/L so the evaporator can 'work at ease.'
II. Machining Wastewater with Metal Chips and Dust
A scraper evaporator is not afraid of sand and mud, but of hard particles.
The gap between scraper and cylinder wall is only 1–3 mm; sharp hard particles like aluminum and iron chips wear the rotor scraper and the heat-transfer cylinder—worn scraper, uneven film, local dry wall, irreversible loss of heat-transfer capacity. This bill is not a cleaning fee but an overhaul fee.
Pretreatment scheme: a few-hundred-yuan basket filter (0.5–1 mm) stops the metal chips and protects the hundreds-of-thousands rotor.
III. High-Surfactant Wastewater (Most Easily Overlooked)
Cutting-fluid and cleaner wastewaters with anionics of one or two thousand easily enter the evaporator and do one thing: foam.
Foam escapes with the secondary steam, maxing out the demister load and clouding the condensate with entrained liquid; in severe entrainment, the MVR compressor impeller bears the brunt.
Pretreatment scheme: continuous defoamer addition on the feed line plus a high-spec demister on the evaporator—don't wait for the foam to rise before remedying.
IV. High-Hardness, High-Silica Wastewater
TDS is not the scare; Ca2+ and SiO2 are. Once the concentration multiple goes up, calcium carbonate and silica scale precipitate on the heat-transfer surface; scaling rate vs. concentration multiple is exponential—nothing for the first 5x, sudden blowout at the 8x.
Pretreatment scheme: for feed hardness > 500 mg/L, softening or scale inhibitor is recommended, and design margin should be reserved for the concentration multiple.
V. High-Chloride Wastewater
Cl- itself is fine if not high (a few hundred), but it enriches in the concentrate: raw water 400, concentrated 10x becomes 4000; under scouring + high temperature + acidic conditions, 304 cannot hold and 316L is also shaky.
Pretreatment scheme: report the chloride ions when doing the water-quality assessment; upgrade material to duplex steel where due, or cap the concentration multiple—wrong material is the number-one cause of low-temperature evaporation project rework.
A Summary Table
| Water-Quality Characteristic | Consequence of No Pretreatment | Pretreatment Measure |
| Oil content > 1000 | Oil-film scaling, oily effluent | Dissolved-air flotation / demulsification de-oiling |
| Contains metal chips | Scraper wear, irreversible heat-transfer drop | Basket coarse filtration |
| Surfactant > 500 | Foaming with entrained liquid, exceeding effluent | Defoamer + demister |
| High hardness & high silica | Exponential scaling blowout | Softening / scale inhibitor |
| High chloride ions | Equipment corrosion and scrap | Material upgrade / control concentration multiple |
Low-temperature evaporation is not about buying one piece of equipment, but a system of 'water-quality diagnosis -> pretreatment -> evaporation main unit -> concentrate outlet.' The pretreatment money, a tiny fraction, decides the life of the multi-million equipment.
Which type is your wastewater? Drop the water-quality indicators in the comments and I will check whether it can go straight to evaporation and which steps to do first.